From Lab Discovery to Digital Printing: The Real History of Sublimation Sportswear
The Evolution of Sublimation Printing: From 1950s Chemistry to Modern Sportswear
Table of Contents
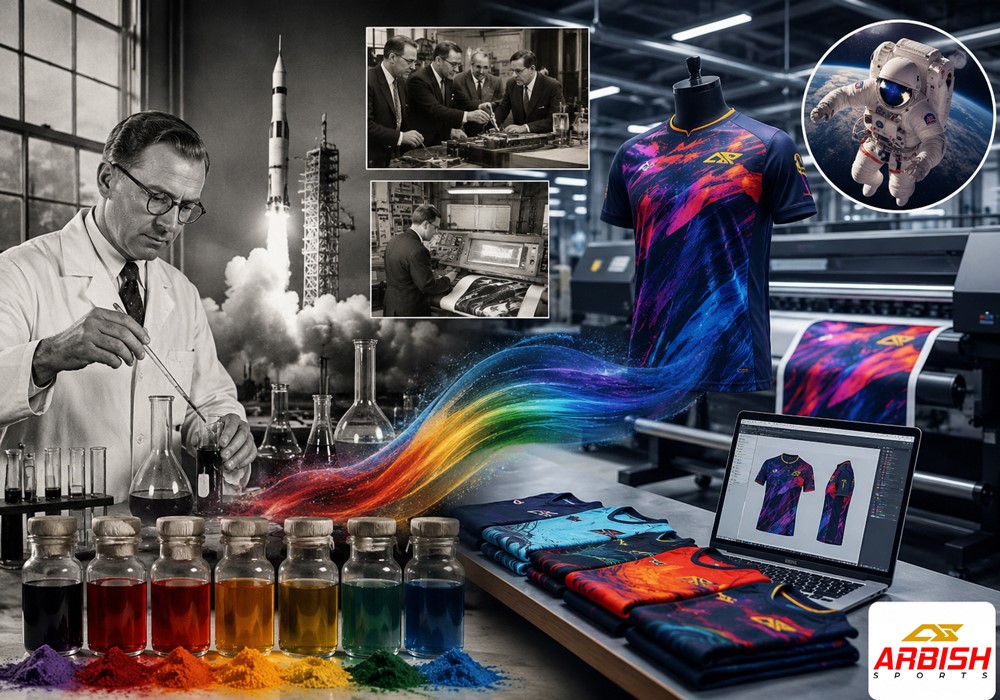
ToggleThe history of sublimation is very interesting. Sublimation printing started as a lucky lab discovery in France in 1957. A researcher named Noël de Plasse found that some dyes could turn straight into gas without ever becoming liquid. That single discovery grew into the process that now prints thousands of custom jerseys, jackets, and uniforms every single day.
The path from paper transfers to full-color digital printing took decades. It moved through French textile mills, then jumped to NASA’s Jet Propulsion Lab, then landed in modern factories that print full uniforms in a single pass. Today, brands like Arbish Sports use this same science, just faster, sharper, and far more precise, to build custom athletic gear at scale.
This article walks through that full journey. We’ll compare old methods to new ones, explain the chemistry in plain words, and show why this history still matters for anyone buying custom sportswear today.
What Is Sublimation, Really?
Before the history, here’s the science in one sentence.
Sublimation is when a solid turns directly into a gas, no liquid step in between.
Think of dry ice. It doesn’t melt into a puddle. It just smokes away into the air. Certain dyes do the same thing when heated. And when that dye-gas hits polyester fabric, something interesting happens.
- Heat opens up the tiny pores in polyester fibers.
- The gas slips inside those open pores.
- As the fabric cools, the pores close and trap the color inside.
The dye doesn’t sit on top of the shirt like regular ink. It becomes part of the fabric. That’s why sublimated designs don’t crack, peel, or fade the way screen-printed graphics can.
1957: The Accidental Discovery That Started It All
Noël de Plasse and Lainière de Roubaix
In 1957, a French researcher named Noël de Plasse was working for a textile company called Lainière de Roubaix. He was testing dyes when he noticed something odd. Under high heat, certain solid dyes skipped the liquid stage completely and turned into gas.
This wasn’t something he set out to find. It was a side discovery, the kind that changes an entire industry by accident.
De Plasse quickly saw the bigger picture. If dye could turn into gas, and if that gas could soak into fabric, he could print designs that would never wash out or crack off. He had just discovered dye-sublimation printing.
The Birth of Sublistatis SA
De Plasse didn’t sit on his discovery. He helped found Sublistatis SA, a company built specifically to turn this lab finding into a real commercial process.
Sublistatis SA is the reason sublimation didn’t stay a curiosity. The company pushed the technique into factories and mills across Europe, turning a chemistry trick into an actual manufacturing method.
By the late 1960s, transfer paper made using this process was rolling off production lines. And by 1970, the industry had produced around 24 million square meters of transfer paper. A few years later, that number jumped to roughly 350 million meters a year, with about a third of all printed polyester using the transfer method.
How Early Sublimation Actually Worked
The first version of sublimation printing was a two-step, paper-based process. It’s important to understand this step because it’s the direct ancestor of what happens in a modern print shop today.
Step 1: Print on paper. A design was printed onto special transfer paper using dye-based ink.
Step 2: Heat press the transfer. That paper was pressed against polyester fabric using heat and pressure. The dye turned to gas, passed into the fabric, and bonded there permanently.
This method worked, but it had real limits.
| Early Sublimation (1960s–70s) | Limitation |
|---|---|
| Design printed on paper first | Extra step, extra material cost |
| Manual heat press setup | Slower, more labor per unit |
| Limited color range | Fewer available dye colors |
| Mostly flat, simple patterns | Hard to do photo-quality designs |
| Analog, non-digital process | No way to easily customize per order |
This was good technology for its time. But it wasn’t built for mass customization, the kind sports teams and brands need today.
The NASA Connection: Wes Hoekstra and Computer-Driven Printing
Here’s the part of the story most people don’t know.
The next big leap for sublimation didn’t happen in a textile mill. It happened at NASA’s Jet Propulsion Laboratory (JPL) in Pasadena, California.
From Space Images to Sublimation Ink
Wes Hoekstra worked at JPL on image processing, the kind of work used to clean up and analyze pictures sent back from space missions. While working on that technology, Hoekstra realized the same digital image-processing principles could drive a sublimation printing system.
Instead of printing designs by hand onto transfer paper, a computer could now control the entire printing process. This was a genuine breakthrough. It’s why Hoekstra earned the nickname “father of the computer image sublimation industry.”
Why This Mattered
Before Hoekstra’s work, sublimation was analog. Every design change meant new plates, new setups, and slow manual work.
Computer-driven sublimation changed that completely.
- Designs could be created and edited digitally.
- Printers could reproduce complex images, not just simple patterns.
- Color accuracy improved dramatically.
- Small production runs became realistic, not just mass runs.
This is the moment sublimation stopped being just a textile trick and started becoming a true digital printing technology.
Comparing the Two Eras: Paper Transfer vs. Digital Inkjet
It helps to see the two major eras side by side.
| Feature | Paper Transfer Era (1957–1970s) | Digital Inkjet Era (1980s–today) |
|---|---|---|
| Design input | Hand-drawn or analog plates | Computer software |
| Print method | Paper printed, then heat pressed | Direct or transfer inkjet printing |
| Color accuracy | Limited, inconsistent | High precision, full color range |
| Customization | Slow, expensive per change | Fast, cheap per design change |
| Speed | Manual, labor-heavy | Automated, high-volume capable |
| Best use case | Basic patterns, bulk fabric | Photo-realistic designs, custom uniforms |
This table shows why modern sportswear brands can now offer full-color, name-and-number custom jerseys for individual players, something totally out of reach with 1960s equipment.
Why Polyester Made This All Possible
Sublimation only works well on synthetic fabric, mainly polyester. This isn’t a small detail. It’s actually central to the whole story.
The Fabric-Chemistry Match
Polyester fibers have a structure that opens up under heat and closes back down as it cools. Natural fibers like cotton don’t behave this way. Their structure doesn’t “breathe” the same way under heat, so dye gas can’t lock in the same manner.
This is why:
- Sports jerseys are almost always polyester or a poly-blend.
- Cotton shirts use different printing methods, like screen printing or DTG (direct-to-garment).
- Performance fabric innovation and sublimation printing grew up together, not separately.
As polyester fabric technology improved, better weaves, moisture-wicking blends, lighter weights, and sublimation printing improved right along with it. One innovation fed the other.
From JPL to the Factory Floor: Digital Textile Printing Today
Modern sublimation printing looks nothing like the 1960s process, even though the core chemistry is identical.
Modern Workflow
- Design digitally. Graphics are built in software with exact colors, logos, and player numbers.
- Print with large-format inkjet. Sublimation ink is printed directly onto transfer paper using industrial inkjet printers.
- Heat press onto fabric. The printed paper is pressed onto cut fabric panels using calibrated heat and pressure.
- Cut and sew. The now-printed fabric is cut into pattern pieces and sewn into finished uniforms.
This is a world away from the manual plate work of the 1960s. What used to take days of setup can now happen in hours, with far better accuracy.
Why This Matters for Athletic Brands
For B2B buyers, teams, leagues, manufacturers, and athletic brands, this evolution means:
-
- Full-color designs are now standard, not a luxury upgrade.
- Individual player customization (names, numbers, sizes) is fast and affordable.
- Colors stay accurate from the first jersey to the five-hundredth.
- Small custom orders are no longer a manufacturing headache.
This is exactly the kind of production capability that companies like Arbish Sports rely on when producing custom team uniforms at scale.
A Quick Timeline
| Year | Event |
|---|---|
| 1957 | Noël de Plasse discovers dye sublimation at Lainière de Roubaix |
| Late 1950s | Sublistatis SA founded to commercialize the process |
| Late 1960s | Transfer paper production using ribbons begins |
| 1970 | Around 24 million square meters of transfer paper produced |
| Mid-1970s | Production surges to roughly 350 million meters annually |
| 1970s | Wes Hoekstra at NASA JPL develops computer-driven sublimation |
| 1980s–90s | Digital inkjet sublimation grows across the textile industry |
| Today | Full-color, on-demand digital sublimation powers custom sportswear |
Why This History Still Matters for Buyers Today
It might seem strange to care about a 1957 lab discovery when you’re just trying to order team jerseys. But understanding this history actually helps buyers make smarter decisions.
It explains why sublimated fabric doesn’t crack or peel. The dye is inside the fibers, not sitting on top, a direct result of de Plasse’s original chemistry.
It explains why polyester blends matter. Manufacturers didn’t pick polyester randomly. It’s the fabric that makes the entire sublimation process work.
It explains why digital customization is now affordable. Without Hoekstra’s computer-driven system, individual player names and numbers would still be a slow, expensive add-on instead of a standard feature.
When a brand talks about “full sublimation printing” today, they’re really describing seventy years of layered innovation, French chemistry, American computer science, and decades of fabric engineering, all working together in one heat press.
From a French Lab to Modern Sportswear
The 70-year journey of dye-sublimation printing, from a 1957 chemistry accident to today's digital textile printing.
The Basic Chemistry
One rule makes the whole process work: solid dye turns straight into gas, then locks into fabric fibers.
Solid Dye
Dye starts as a solid, printed onto transfer paper.
Heat + Gas
Heat turns the dye into gas — no liquid stage at all.
Locked in Fiber
Gas enters polyester fibers, which seal shut as they cool.
The Timeline
Two countries, two breakthroughs, one printing process.
Noël de Plasse's Discovery
At Lainière de Roubaix, de Plasse finds that certain dyes turn from solid straight to gas under heat.
Sublistatis SA Founded
A company forms to turn the lab discovery into a real commercial printing process.
Wes Hoekstra at NASA's JPL
Using image-processing know-how from space missions, Hoekstra builds the first computer-driven sublimation system.
Digital Inkjet Sublimation
Full-color, on-demand printing makes custom team uniforms fast and affordable.
Then vs. Now
The chemistry never changed. The speed and precision did.
Paper Transfer Era
- Hand-set analog plates
- Manual heat press setup
- Limited color range
- Slow, costly design changes
Digital Inkjet Era
- Full-color computer design
- Automated inkjet printing
- Photo-realistic accuracy
- Fast, affordable small runs
Why Polyester Makes It Work
Heat opens polyester fibers so dye-gas can enter, then seals them shut on cooling. Cotton doesn't open the same way — that's why sports uniforms are almost always polyester.
Seventy Years of Innovation, One Uniform
See how modern digital sublimation brings sharp, durable custom designs to your team's gear.
Explore Arbish Sports CollectionsFAQ
What is dye sublimation printing?
Who invented sublimation printing?
Who created computer-driven sublimation printing?
Why does sublimation only work well on polyester?
Is sublimation printing better than screen printing for sports uniforms?
Can sublimation printing handle small custom orders, like a single team roster?
Ready to Put This Technology to Work?
Seventy years of innovation, from a French lab in 1957 to NASA’s image-processing labs, now sits behind every custom jersey, warm-up kit, and team uniform on the market. That history is exactly why modern sublimation printing delivers sharp colors, durable fabric, and true one-player customization.
If you’re an athletic brand or manufacturing client looking to put this proven technology to work, browse Arbish Sports’ custom sportswear collections. Explore the product category pages to see how modern digital sublimation can bring your team’s designs to life with the accuracy and durability this seventy-year-old science was built to deliver.